
Capabilities
Pi Fabricators
Family-owned fabrication and machine shop in Salem, Oregon, founded in 2019 by Nick and Daniel Bechtoldt. We build to print, and we can redesign the part on the way through — a licensed Professional Engineer is one of the two owners. Wear parts, weldments and machined components for mills, recyclers and processors across the Pacific Northwest.
CNC machining
- Doosan DNM 5700 VMC with 4th axis — BT40 BIG-PLUS 8,000 rpm spindle, 30-tool changer, through-spindle coolant, FANUC 0i
- Summit 19 × 80 engine lathe — 27 in swing over the gap, 4-1/8 in spindle bore, inch & metric threading
- Renishaw probing; keyways, bores and multi-sided parts in one setup; tolerances quoted per part and material
Fabrication & welding
- MIG & TIG welding — carbon steel and stainless
- Custom weldments, structural assemblies, heavy-wall pipe, auger flight welding, repairs
- In-house forming on a 90-ton × 12 ft press brake, used to support our fab processes
- Jib crane and custom fixturing for large and awkward parts
Engineered wear solutions
- CNC-controlled thermal spray hardfacing — nickel superalloy, chrome carbide, tungsten carbide; spray-and-fuse in a controlled-atmosphere furnace; service to 1,200 °F+
- MIG tungsten-carbide embedding — WC particles in a weld matrix for debarker flights, auger tips, glass-breaker skirts
- Weld-overlay hardfacing — chrome carbide for compaction tubes, hog grates, wear plates
- Deposit hardness per consumable data sheet: chrome carbide overlay 63–67 HRC; WC-embed matrix 58 HRC with 70 HRC carbide
Surface prep, finishing & heat treatment
- Abrasive blast cabinet — crushed and spherical steel shot; profiling, coating removal, shot peening
- Tumble blaster and centrifugal barrel tumbler — batch deburring, descaling, edge radiusing
- Controlled-atmosphere furnace — vacuum pump-down, argon/hydrogen atmosphere, to 1,960 °F: spray-and-fuse, scale-free annealing and stress relief of weldments
Quality & engineering
- Daniel Bechtoldt, PE — Oregon Professional Engineer #89334; design, analysis and redesign for longer life
- 4 × 6 ft precision granite surface plate; bore, height, thread and micrometer inspection to your drawing
- Single point of contact for partner processes: line boring, hard chrome plating, custom pipe bending
Service & terms
- Quotes within 2 business days — pifabricators.com/pages/quote
- One-off repairs to production runs
- Salem, OR — serving the Pacific Northwest; ships nationwide
- Net 30 on approved credit; new accounts may be asked for a deposit. Credit card and check accepted.

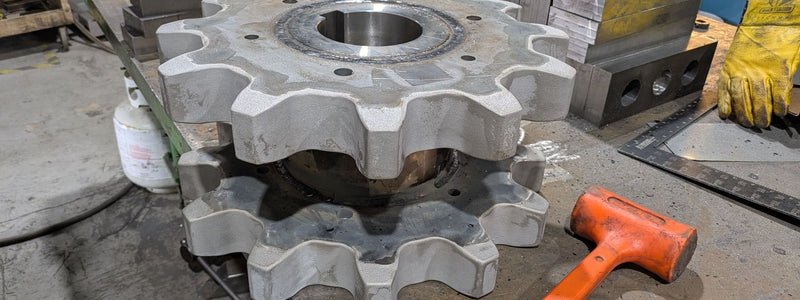
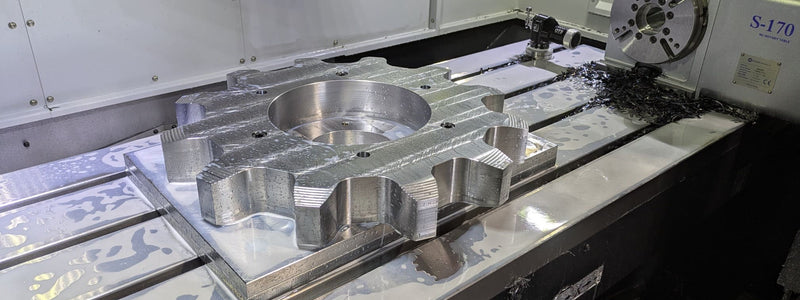
Engineering on the way through
Daniel Bechtoldt, PE co-owns and co-operates the shop, so a part can be analysed and redesigned as it goes through — not just fabricated to print. Recent examples: a single-piece auger redesigned as a maintainable assembly with a removable tip; heavier-duty compaction tubes engineered to take hardfacing with acceptable warpage.
Equipment detail
- Doosan DNM 5700 — FANUC 0i-M control, 4th-axis rotary for keyways and multi-sided parts, through-spindle coolant
- Summit 19 × 80 lathe — D1-8 camlock spindle, 12 speeds 22–1,500 rpm, 7.5 hp, taper attachment, steady and following rests, 3- and 4-jaw chucks
- Blast cabinet — surface profiling, coating removal, pre-weld cleaning, shot peening
- Tumble blaster and centrifugal barrel tumbler — pre- and post-weld prep, paint prep, fatigue-life enhancement
- Inspection — bore, height and thread gauges, micrometers and calipers on a 4 × 6 ft granite surface plate
Partner network
For processes outside the shop — precision line boring, hard chrome plating, custom pipe bending — we work with a trusted network of manufacturing partners and manage the relationship and the quality, so you have one point of contact through the whole project.